A Code Stamp Is an Entity, Not a Badge
Nearly every welding and vessel shop I look at owns something its marketing throws away. The code stamps. ASME U, National Board R, AWS qualifications, the whole compliance file that took years and real money to earn, sitting in a row of gray logo images at the bottom of the homepage.
Here is what that row actually is. Each mark is a third-party attestation with an issuing body, a defined scope, a certificate number, and an expiration date. That combination makes it an entity fact instead of an adjective. A buyer can verify it. A language model can match it. "Quality workmanship" can be neither verified nor matched, which is why it does nothing for a shop in either channel.
That split decides who gets found in
welding and fabrication marketing. One kind of statement survives contact with a filter. The other evaporates. The rest of
manufacturing marketing has the same habit of leading with adjectives, but code-gated work punishes it harder. A shop without the right authorization is not a cheaper option. It is not an option.
The Certifications Buyers Filter On
Procurement builds a bid list by elimination. Before anyone reads a capability page, someone runs a gate: does this shop hold the authorization the job requires, and is it current.
The marks that show up on those gates:
- ASME U, U2, and U3, covering new pressure vessel construction under Section VIII, Divisions 1, 2, and 3
- ASME S, for power boiler work under Section I
- ASME PP, for power piping
- National Board R, for repairs and alterations to pressure-retaining items under the NBIC
- National Board registration of the finished vessel, which is mandatory in most North American jurisdictions
- AWS D1.1 for structural steel, D1.5 for bridges, D1.6 for stainless
- AWS Certified Welding Fabricator, which certifies the shop rather than the individual welder
- A Certified Welding Inspector on staff, or the name of the third party doing the inspecting
- ISO 9001
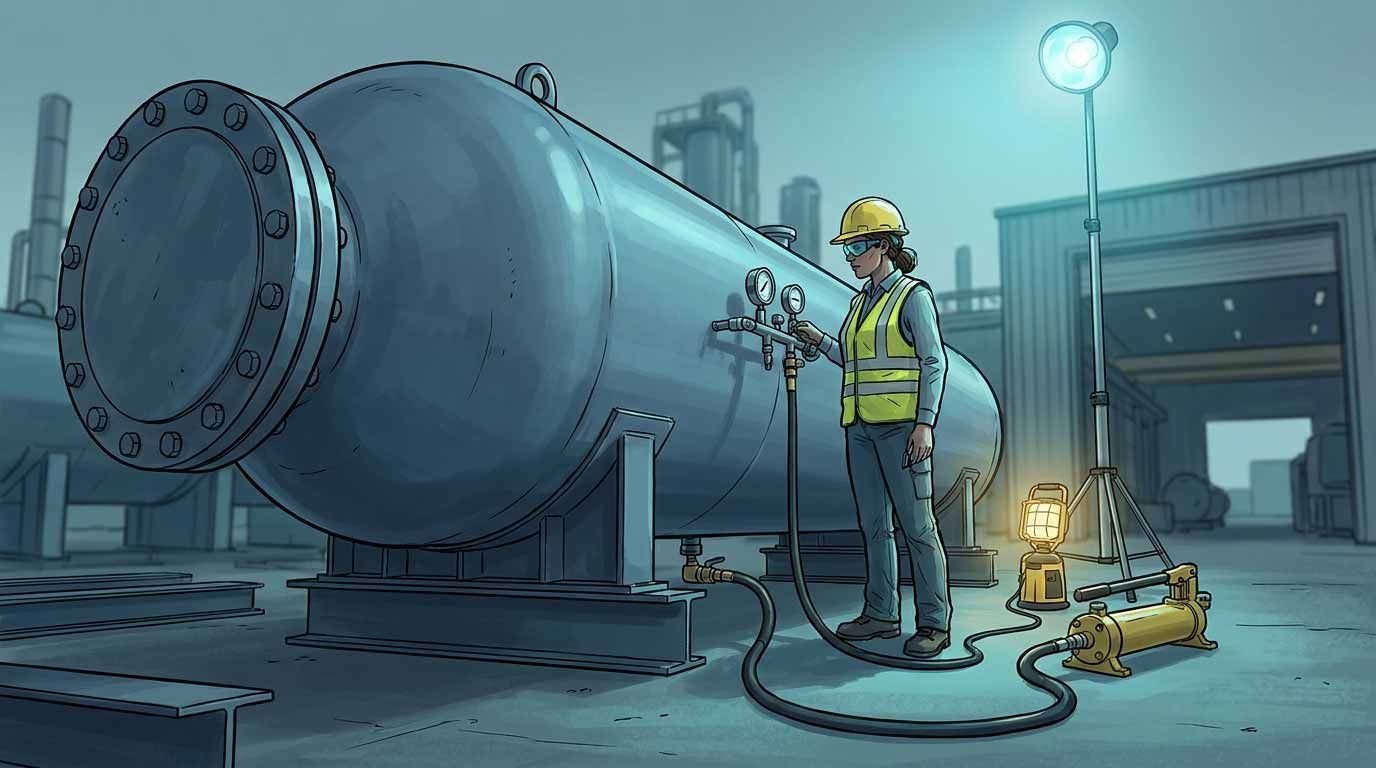
- NDE methods available in house, named one by one: RT, UT, PT, MT, VT, and hydrostatic testing
Every line there is a discrete, sourced, expiring fact. That is the exact shape
structured data through schema markup was built to carry, and it is why
pressure vessel and tank fabricators get more out of a certifications page than almost anyone else in industrial marketing. The information is already precise. It just has to be written down somewhere a machine can read it.
"ASME Certified" Is Where the Scope Disappears
Two words, and a shop erases the difference between building a new vessel, repairing an existing one, and touching a boiler.
Those are separate authorizations with separate scopes and separate audit cycles. An engineer sourcing an alteration to an in-service separator needs an R stamp holder, and a U stamp does not answer that question. When the site says "ASME certified," the engineer either picks up the phone or moves to the next shop, and I know which one happens more often on an afternoon with six vendors to screen.
Scope collapse is the cheapest thing on this list to fix. Name the section. Name the division. Name the body that issued the authorization.
Procedure and Welder Qualifications Belong on the Site Too
The stamps get whatever attention a shop gives this. The qualification records behind them usually get none, and they answer the questions that decide the job.
A shop qualified under ASME Section IX holds welding procedure specifications, procedure qualification records, and welder performance qualifications. Those documents state which processes the shop is qualified to run, which base material groups, which thickness and diameter ranges, and which positions. GTAW root with SMAW fill on P-No. 8 stainless in the 6G position is a capability statement. "Experienced welders" is a mood.
I am not suggesting anyone publish the quality manual. Publish the envelope. Processes, material groups, thickness range, positions, and the code the qualification was written to. That is four lines of a table and it disqualifies fewer jobs than silence does.
Publishing the Code Book
None of this requires new equipment or another audit. It is a writing and structure job. Give each authorization a named place on the site with the issuing body, the code reference, the scope, and the renewal cycle stated in plain sentences. Then mark it up so engines read the facts directly instead of inferring them from a logo file with no alt text.
The shops that win these searches are rarely the ones holding more stamps. They are the ones that treated the certificate file as source material and wrote it out.
How Mansfield Can Help
Mansfield Marketing works with welding shops, fabricators, and pressure vessel builders to turn code stamps, welder qualifications, and inspection capability into published, structured content that procurement teams and AI search engines can both act on. Contact Mansfield Marketing to discuss publishing your shop's ASME and AWS credentials where buyers and engines are actually looking by
requesting a quote or calling us at (713) 936-5557.