What Tier 1 Buyers Actually Evaluate
OEM supply chain managers and sourcing engineers don't browse supplier websites informally. They're working through structured qualification processes with specific documentation requirements that begin long before a shop produces a single part. What I observe is that PPAP and APQP familiarity serves as a first filter. A supplier that can't articulate Production Part Approval Process expectations, including what Level 3 submission involves, signals immediately that they haven't worked at this level.
Mold manufacturers competing for Tier 1 tooling contracts face a specific version of this challenge. The sourcing conversation isn't about price. It's about production readiness, and the questions are specific: has this shop supported APQP timelines with a Tier 1 or Tier 2 customer? Have they gone through formal tool runoff and sample approval? Does their quality system address customer-specific requirements? What I see on
manufacturing websites is that many mold shops don't answer any of these questions.
Tier 1 buyers also distinguish between long-term tooling partnerships and spot sourcing. A shop positioned only for spot work won't attract program partnership inquiries, because nothing on their website signals the operational capacity required for ongoing tooling programs.
What Mold Manufacturers and Tool and Die Shops Need to Communicate
Mold flow analysis and design for manufacturability (DFM) capability are baseline expectations for Tier 1 injection mold programs. Stating that a shop performs Moldflow analysis to verify fill, warp, and cooling performance before steel commitment communicates competence. Stating that they have "experience with complex molds" does not. I notice this distinction matters most early in the sourcing cycle, when engineers are building their short list.
Tool and die shops face a parallel version of this problem. Die type specificity matters. Progressive, transfer, and compound die capabilities aren't interchangeable, and a shop that clearly states which configurations they build and what materials and gauges they run is giving sourcing engineers something to act on. Press tonnage and bed size need to be explicit. "Various press capabilities" tells a sourcing engineer nothing. "50 to 1,200 ton presses, 84-inch bed" tells them whether to move forward.
Content marketing for mold manufacturers and tool and die shops that directly addresses these qualification criteria is what separates shops that reach Tier 1 consideration from those that stay on the generic supplier list.
Tool Steel, Cavity Life, and Die Tolerances
On the mold manufacturing side, tool steel selection affects cavity life ratings and maintenance intervals. The difference between P20, H13, and S7 isn't obvious to everyone in a sourcing department, but engineers evaluating tooling for high-volume programs understand it. A shop that specifies which steels they work in, what hardness ranges they hold, and what cavity life they deliver under stated production volumes is speaking the language Tier 1 buyers respond to.
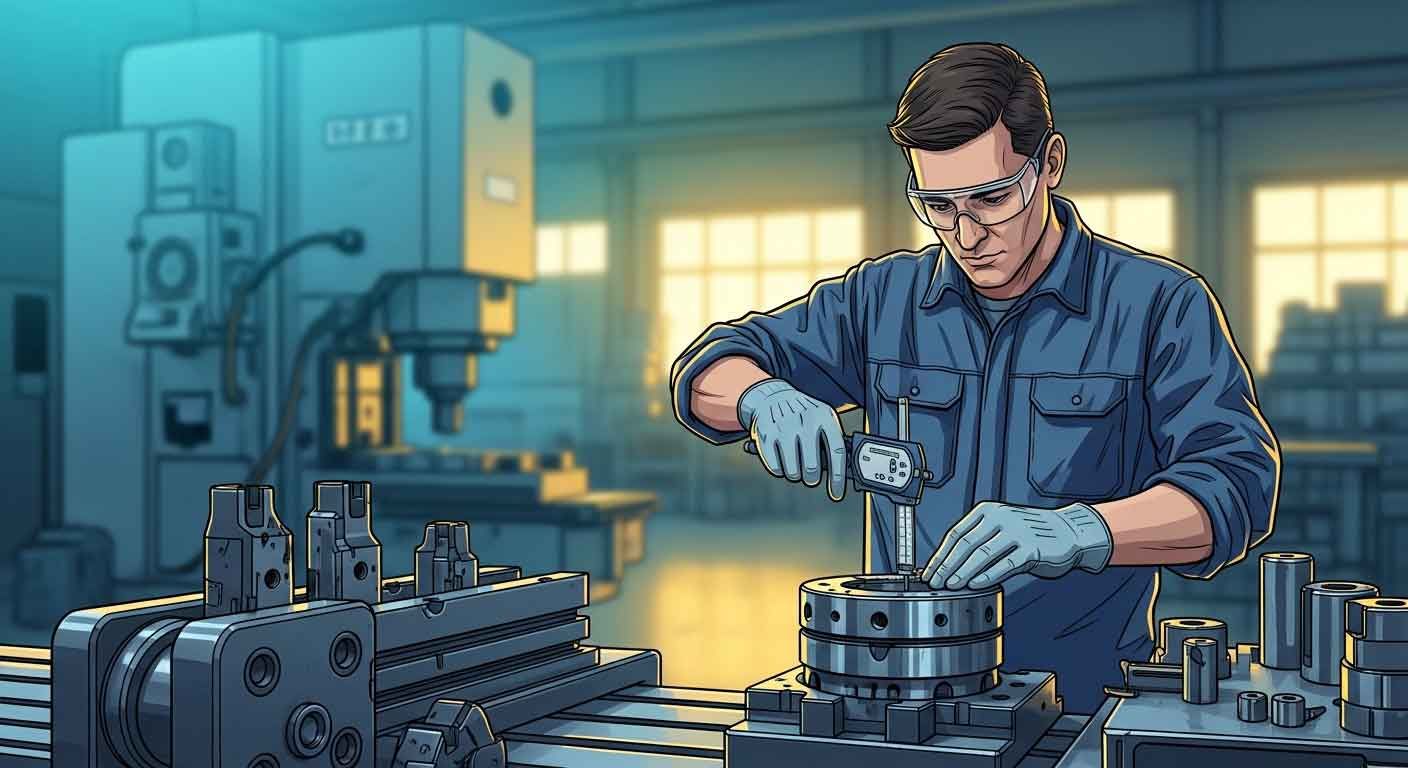
For tool and die shops, tolerances and material range complete the picture. Holding tolerances to ±0.0002 inches on hardened die components and working in D2, A2, and carbide insert tooling is worth stating. "Tight tolerances and experienced team" is not.
Sampling and qualification procedures need to be explicit. What a Tier 1 sourcing engineer wants to find on a capability page:
- T1, T2, and T3 sample build capability with dimensional tracking against nominal
- PPAP submission support including capability studies and material certifications
- Defined runoff procedures before tool transfer or production launch
These aren't questions that get answered after supplier selection. They determine whether a shop makes the approved vendor list in the first place.
Why Generic Positioning Fails with Tier 1 Sourcing Teams
Tier 1 sourcing teams process many tooling suppliers in a given program cycle. What I see across supplier websites is the same language repeated: "precision tooling," "quality craftsmanship," "experienced team." Sourcing engineers can't act on any of it.
They verify. They look for PPAP experience, specific die types, certification documents, and equipment specs. When that information isn't on the website, the shop gets filtered out. Not because they lack capability. Because the marketing doesn't communicate it.
IATF 16949 certification is a good example of where specificity matters more than most shops realize. The certification should appear in the capability narrative, not as a footer badge. And beyond the certification itself, Tier 1 customers impose customer-specific requirements (CSRs) layered on top of IATF 16949. A shop familiar with GM CSRs or Ford-specific quality system requirements needs to say so explicitly. That language, used correctly, signals to a sourcing engineer that this shop has been through this process before.
Building Capability Communications for Tier 1 Consideration
The fix is a structured capability communication strategy that translates shop-floor competence into the language sourcing engineers evaluate. Specific die types named, PPAP documentation support stated, tool steel families listed, quality system certifications front and center in the content where buyers are reading, not relegated to a downloads page.
Shops that do this work attract a different quality of inquiry. The RFQs come from sourcing teams with real programs, not spot buyers shopping on price alone.
How Mansfield Can Help
Mansfield Marketing works with mold manufacturers and tool and die shops to build the capability communications that Tier 1 sourcing teams are actually evaluating. Contact Mansfield Marketing to discuss positioning your tooling business for Tier 1 supplier consideration by
requesting a quote or calling us at (713) 936-5557.